Comparative Review: Precision Molding and Thickness Expectations for Industrial Fiberglass Water Slides
Introduction — a calm comparison
When choosing water park equipment for a new installation, the difference between a slide that lasts and one that becomes a maintenance headache often comes down to molding precision and wall thickness control. I’ll compare common production approaches and show how those choices affect durability, finish, and safety. From my observations around Orlando public parks, tighter tolerances translated to fewer repairs after the first season, which matters if you manage daily operations. The goal here is practical: know which trade-offs matter before you buy water park equipment.
Why molding precision and thickness matter
Precision molding controls how evenly gelcoat and composite layup distribute across a slide’s profile. Even a millimeter of variance in a high-stress elbow will change stress concentration and fatigue life. Good molding limits voids and ensures consistent cure cycle behavior; that reduces delamination risks. In short, consistent lamination and a uniform thickness profile protect both riders and your bottom line.
Comparative techniques: what manufacturers actually do
Three common methods dominate production: hand layup with spray-up, vacuum infusion, and rotational molding. Hand layup is flexible and lower cost but more variable — thickness profiles can fluctuate. Vacuum infusion delivers a dense laminate with fewer voids and more repeatable fiber-to-resin ratios. Rotational molding gives uniform wall thickness in certain geometries but isn’t ideal for long, thin slide sections. Each method brings its own strengths for gelcoat adhesion, mold release agent use, and surface finish.
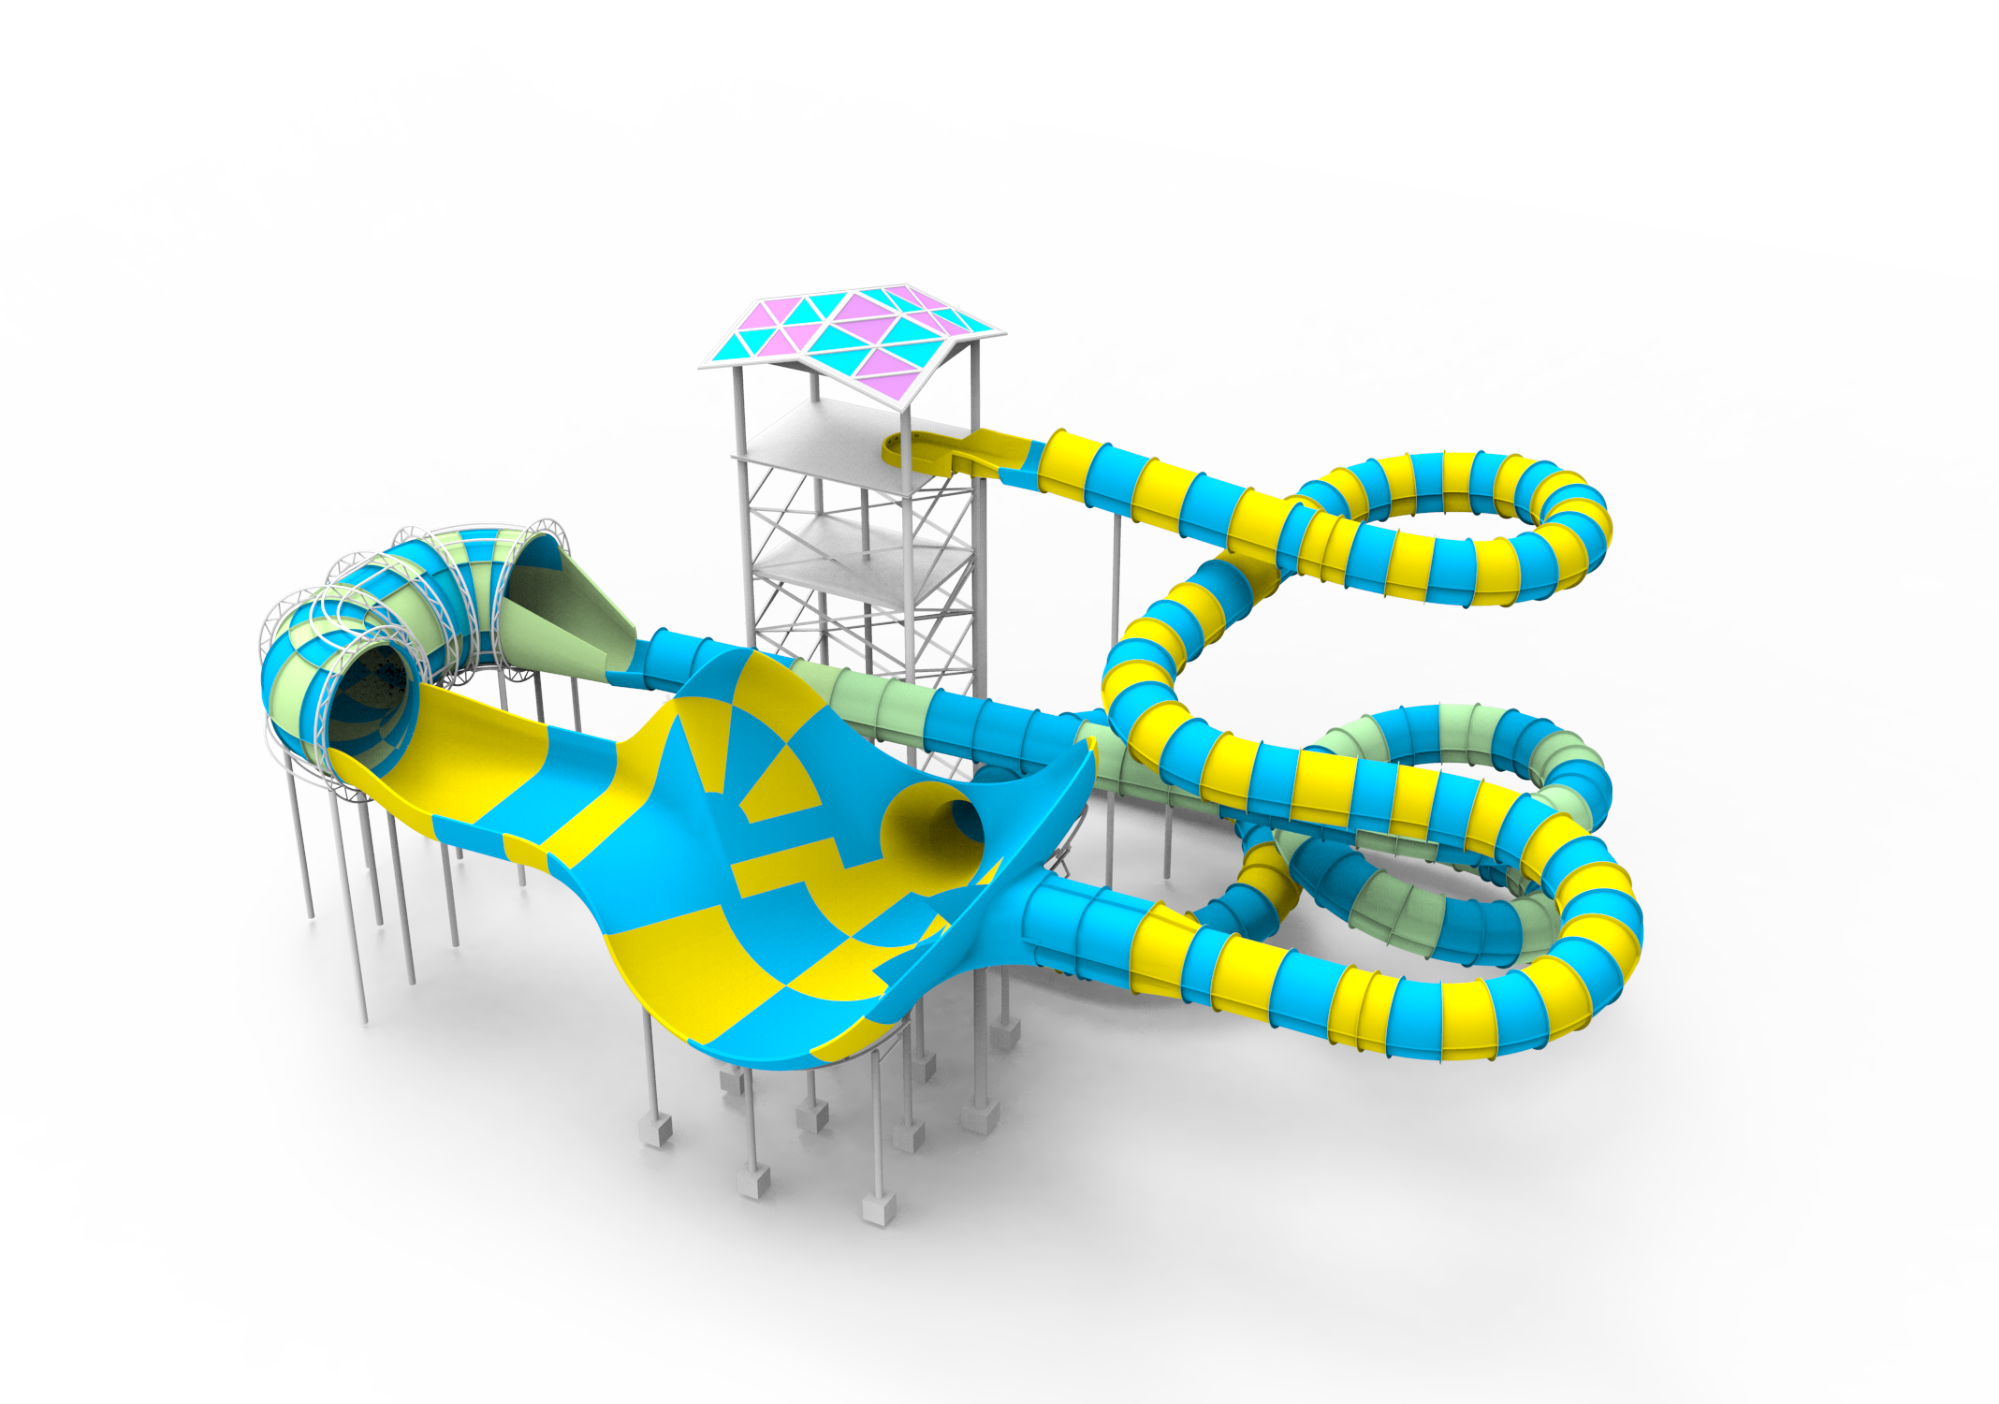 Operational production teardown — practical checkpoints
Here I break down the production run into measurable steps and embed two operational markers: {main_keyword} and {variation_keyword}. Start with the mold: inspect the mold surface for micro-imperfections, because the mold defines the gelcoat finish. Next, verify layup sequencing and fiber orientation; consistent orientation raises impact resistance. Use an ultrasonic thickness gauge to map the finished section; it’s fast and non-destructive. Check cure cycle records so you can confirm the resin reached its specified post-cure temperature for the required period. Finally, sample-cut small sections away from aesthetic surfaces to confirm fiber volume fraction and absence of dry spots.
Common mistakes and mid-life maintenance realities
Manufacturers often skimp on critical tooling tolerances — that’s the source of mismatch at joints and step changes in thickness. Another frequent issue is inadequate post-cure, which leaves resin under-crosslinked and brittle. During operations, UV degradation and surface crazing appear first on thin gelcoat areas; those are the places you’ll need to monitor. Regular inspections with a thickness gauge and simple impact checks catch problems early — and small repairs now prevent large composite repairs later. A note for operators: consistent record-keeping of repairs reduces repeat failures and helps root-cause analysis — it’s worth the effort.
How thickness standards affect design choices
Designers typically target variable wall thicknesses: thicker through elbows and thinner on straight runs. The trick is controlling transitions without sharp steps. Smooth thickness gradients reduce stress risers. If you’re comparing suppliers, ask for a thickness map from sample panels and confirm they measure at consistent intervals. If they can’t produce reliable maps, expect hidden variability. Also, consider how gelcoat thickness ties to abrasion resistance; a modest increase in gelcoat in high-wear zones pays off in longevity.
Choosing between suppliers and alternatives
Compare suppliers by focusing on three concrete metrics: dimensional repeatability, thickness uniformity, and post-cure verification. Alternatives like modular thermoplastic sections can speed installation and offer easier repairs, but they change the ride feel and require different joining techniques. If you favor composites, insist on seeing production QC logs and sample cores. If you prefer thermoplastics, verify joint sealing methods and UV stabilization additives. Both paths work — they just solve different operational priorities.
Advisory — three golden rules for selection
1) Require a thickness map and ultrasonic test report for representative sections; accept nothing less than documented tolerances. 2) Verify cure cycle records that show ramp rates, hold temperatures, and total post-cure time; those parameters determine long-term resin performance. 3) Prioritize suppliers who demonstrate consistent mold maintenance and a schedule for gelcoat touch-up — that small discipline saves downtime.
When those three checks are in place, you get predictable performance from your aquatic playground equipment and lower lifecycle costs. For project teams needing proven systems and steady supply, Dalang often aligns production discipline with practical service — a reliable fit for operators seeking fewer surprises. —